 SPTI · Stroke 001
We Build Quality.
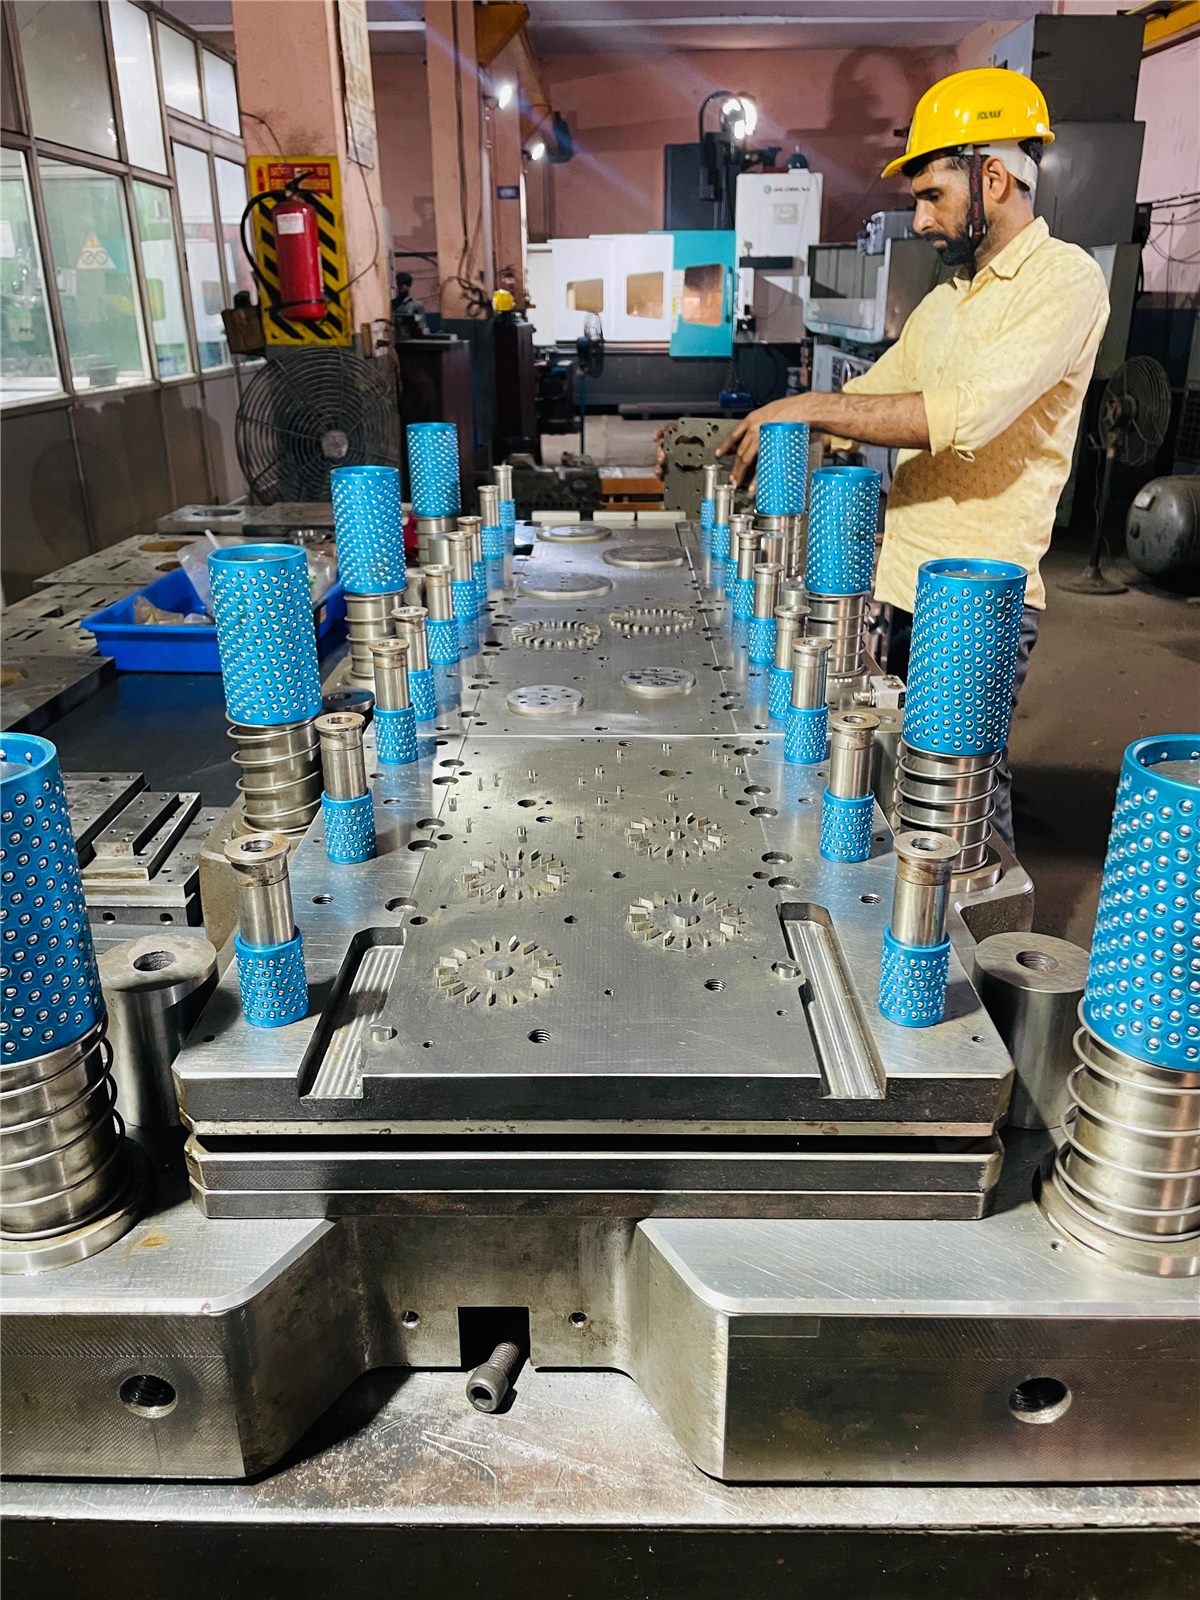
Electrical lamination progressive dies engineered to ±0.005 mm — with in-die AutoStack, AutoSkew and AutoRotation, multi-row layouts and slinky EV stator tooling for motor makers across India.
Two decades of tooling, consolidated into one precision enterprise.
What began in 2007 as a tool-and-die unit is today a modern, innovation-led facility in Faridabad — building the progressive dies that stamp India's motor laminations.
-
2007
Sai Engineering Works founded
Mr. Satbir Singh lays the foundation — a tool & die unit focused on high-quality progressive tooling, rooted in craftsmanship and customer trust.
-
2014
Stampwell Pvt. Ltd. established
A parallel venture producing rotors and stators for clients including Autolek, BCH and Varroc — proving the tooling at production scale.
-
2018
Consolidated as SPTI
Both ventures unite as Sai Precision Tool Industries, specialising in lamination progressive dies with AutoStack and AutoSkew technologies.
-
Today
Modern, innovation-led tooling enterprise
A state-of-the-art facility with Japanese, Swiss and Italian machinery and a team dedicated to quality and customer satisfaction.
Growth trajectory
FY 2007–08 → FY 2024–25 · %To manufacture high-quality, precision-driven products while delivering exceptional after-sales service — creating lasting value for customers, employees, suppliers and the community.
Finished cores, straight out of the die.
Our lamination dies don't just blank parts — they interlock, skew, rotate and coil them in-tool, so customers receive assembly-ready stator and rotor stacks at press speed.
AutoStack
Each lamination is formed with interlock points and pressed onto the one below inside the die. A counting station separates stacks at the programmed height — producing rigid, ready cores without welding, cleating or riveting.
- Benefit
- No secondary stacking
- Proven on
- Ø130.45 stator · 0.9 mm sheet
AutoSkew
The rotor die indexes each lamination by a minute angle as it stacks, building the slot skew into the core itself. Skewed rotors reduce cogging torque, noise and harmonic losses — critical for quiet pumps, fans and EV drives.
- Benefit
- Lower noise & cogging
- Proven on
- EV motor · 0.25 mm sheet
AutoRotation
The stack is rotated between laminations so that natural variation in strip thickness cancels out around the circumference — giving parallel, square cores with uniform stack height and consistent magnetic performance.
- Benefit
- Uniform stack height
- Result
- Parallel, square cores
Slinky EV Stator
Instead of blanking full rings, the stator is stamped as a continuous toothed strip and wound helically into a core. Material utilisation rises dramatically on large-diameter stators — ideal for EV hub and traction motors.
- Benefit
- Far less scrap
- Tooling
- Incl. 4-cavity slinky dies
Multi-Row Layouts
1-, 2-, 3- and 4-row strip layouts nest multiple stator–rotor sets across the coil width, multiplying output per press stroke and squeezing scrap out of every metre of electrical steel.
- Configurations
- 1 · 2 · 3 · 4 Row
- Proven on
- Water pump · 3 Row
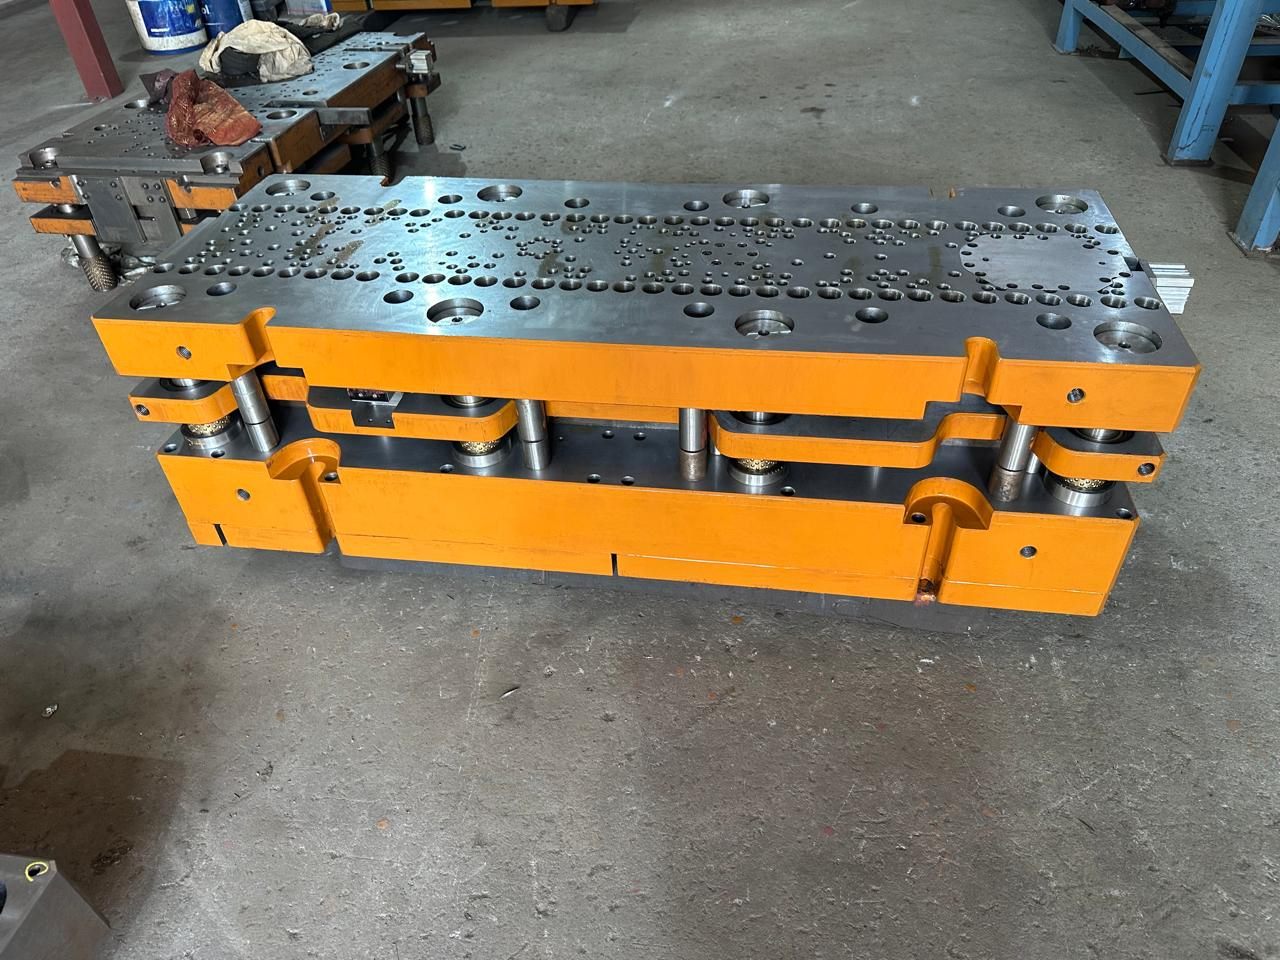
Progressive dies, built and proven in-house.
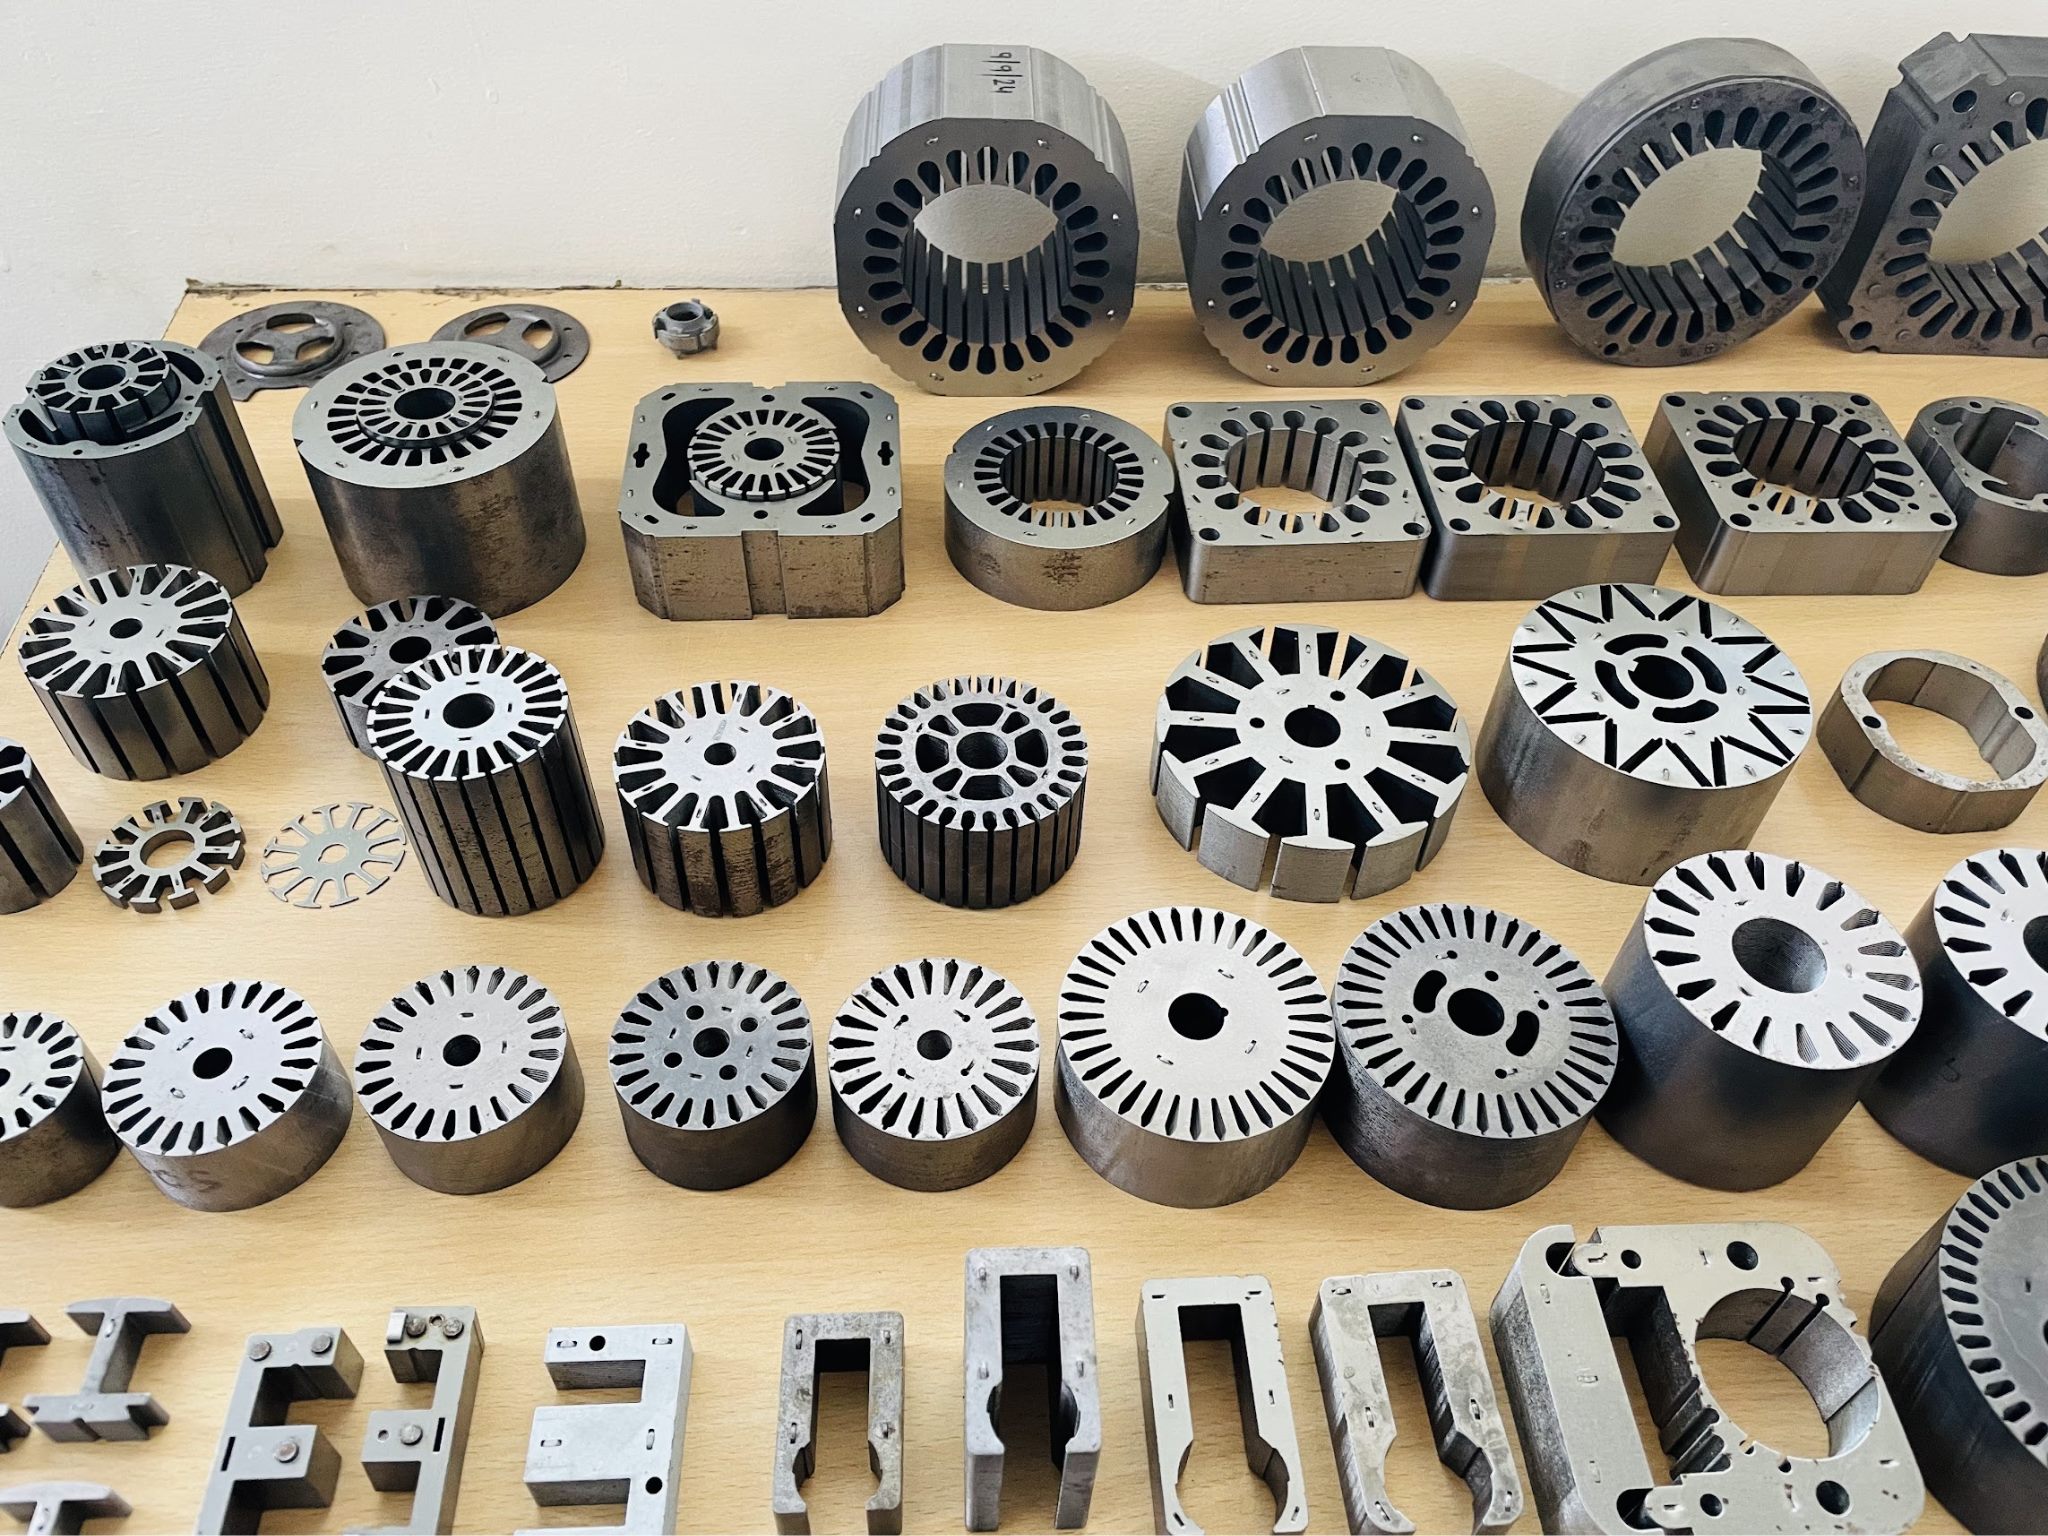
A selection of lamination and specialty dies from our shop — from single-row exhaust-fan tooling to 3-row AutoSkew dies and thin-gauge stainless gasket tools.
Every stroke, identical.
Raw electrical steel in, finished laminations out. Watch an SPTI progressive die running on the shop floor.
The video couldn't be played here. Download the demo video instead.
Strip enters the die
Coil-fed electrical steel advances station by station with pilot-located accuracy.
Slots, bores & interlocks
Stator and rotor geometry is pierced and blanked — rotor inside stator — on every stroke.
Cores leave assembled
AutoStack and AutoSkew stations deliver counted, interlocked cores ready for winding.
Laminations for every motor we touch.
Stators and rotors for BLDC, induction and shaded-pole motors; slinky stators and hubs for EV; and specialised gasket and component tooling.
- Loading products…
Automotive — EV & ICE
Traction and hub-motor laminations, slinky stators and engine gasket tooling.
Domestic appliances
Coolers, water pumps, exhaust and ceiling fans — high-volume, multi-row dies.
Industrial electrical
Electric pump and general-purpose motor laminations for stamping houses.
Swiss, Japanese & Italian precision under one roof.
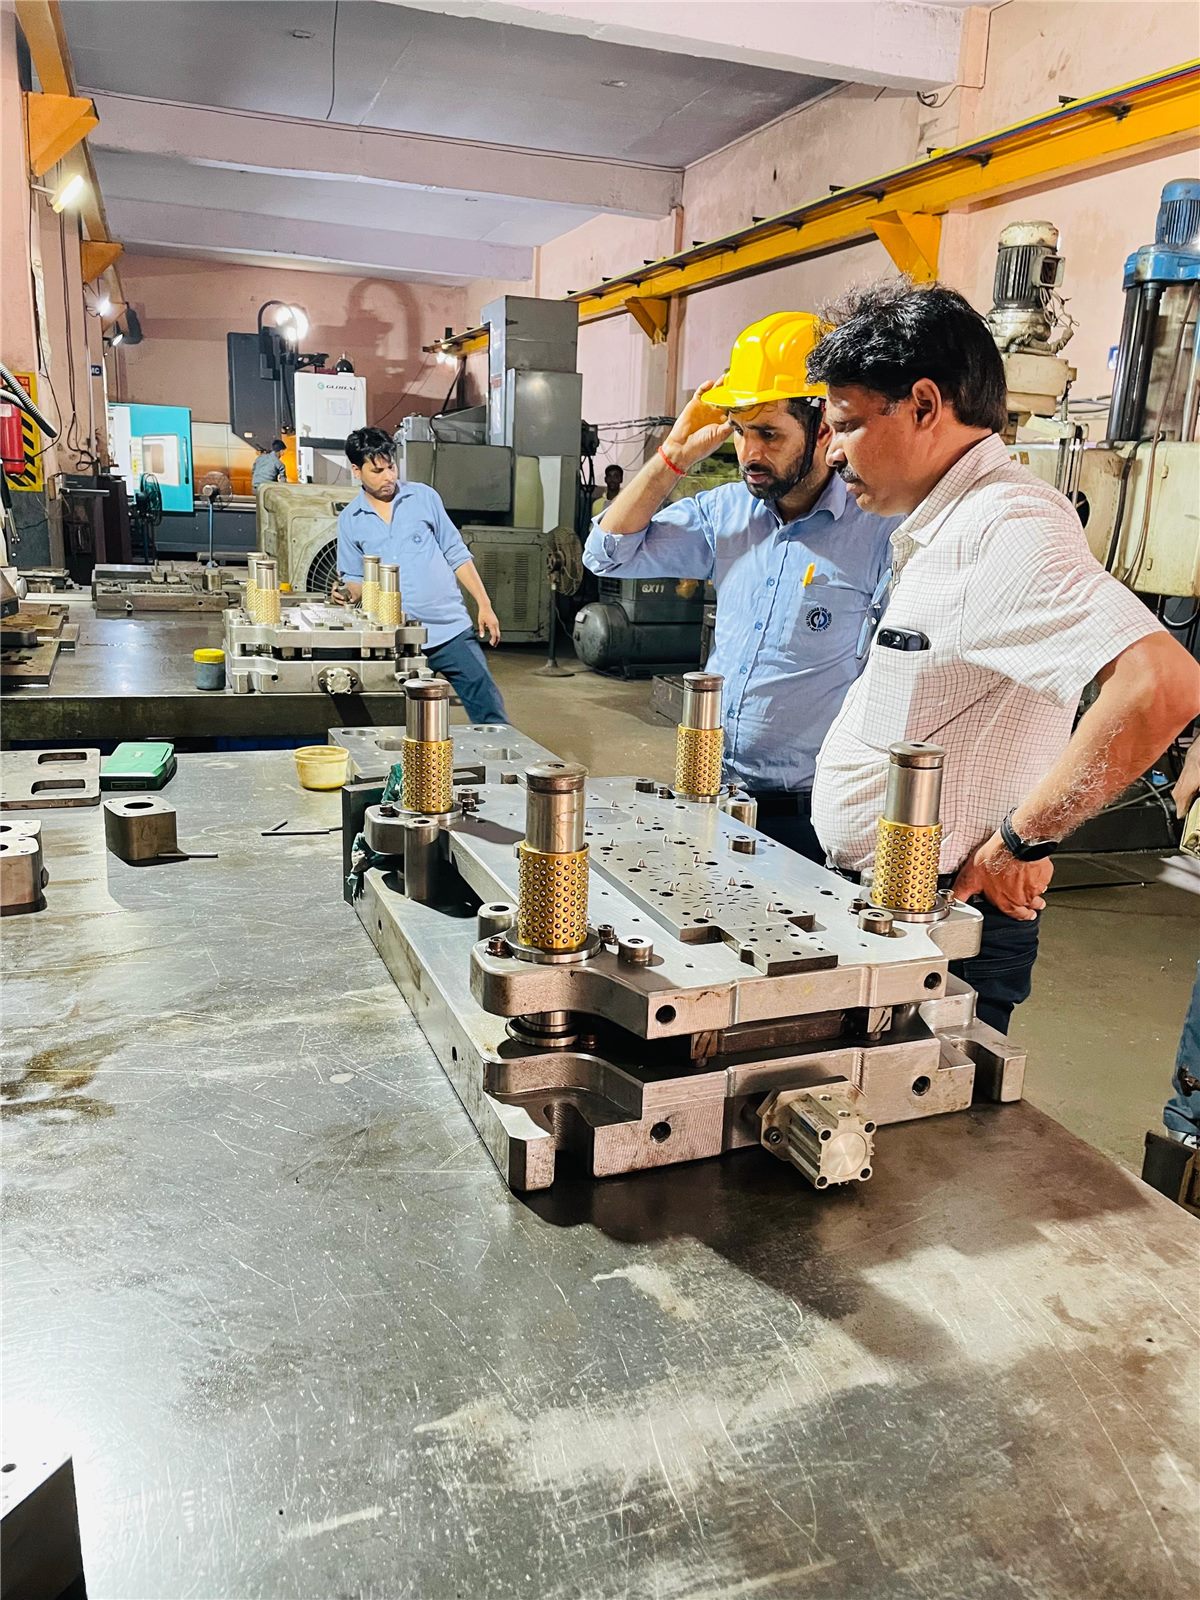
Every die is cut, ground, bored and tried-out in-house — from wire-EDM profiles to high-speed press validation.
Loading machine park…
Measured in microns. Certified by process.
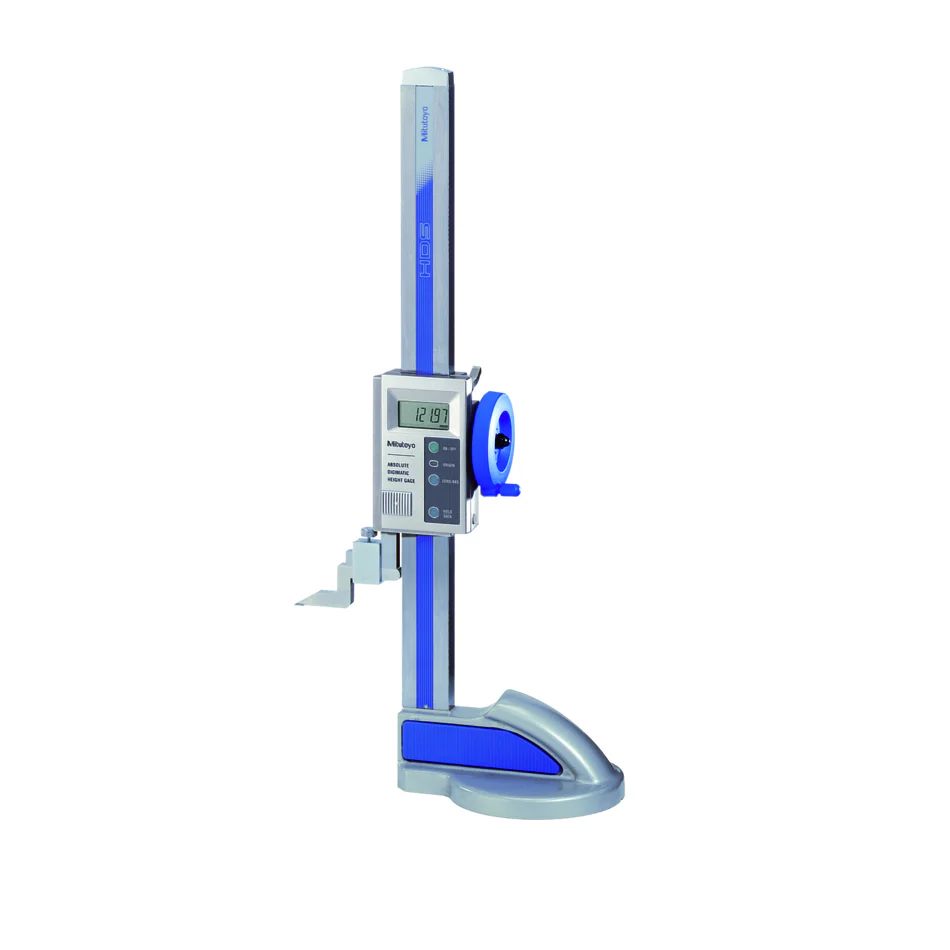
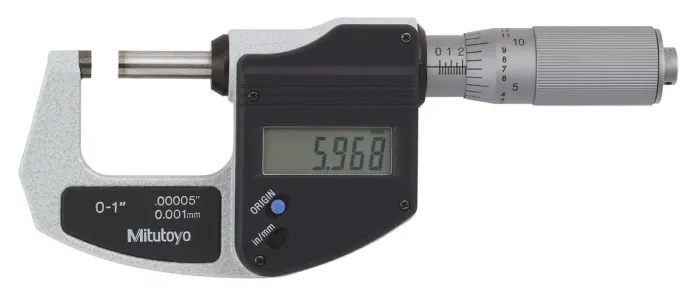
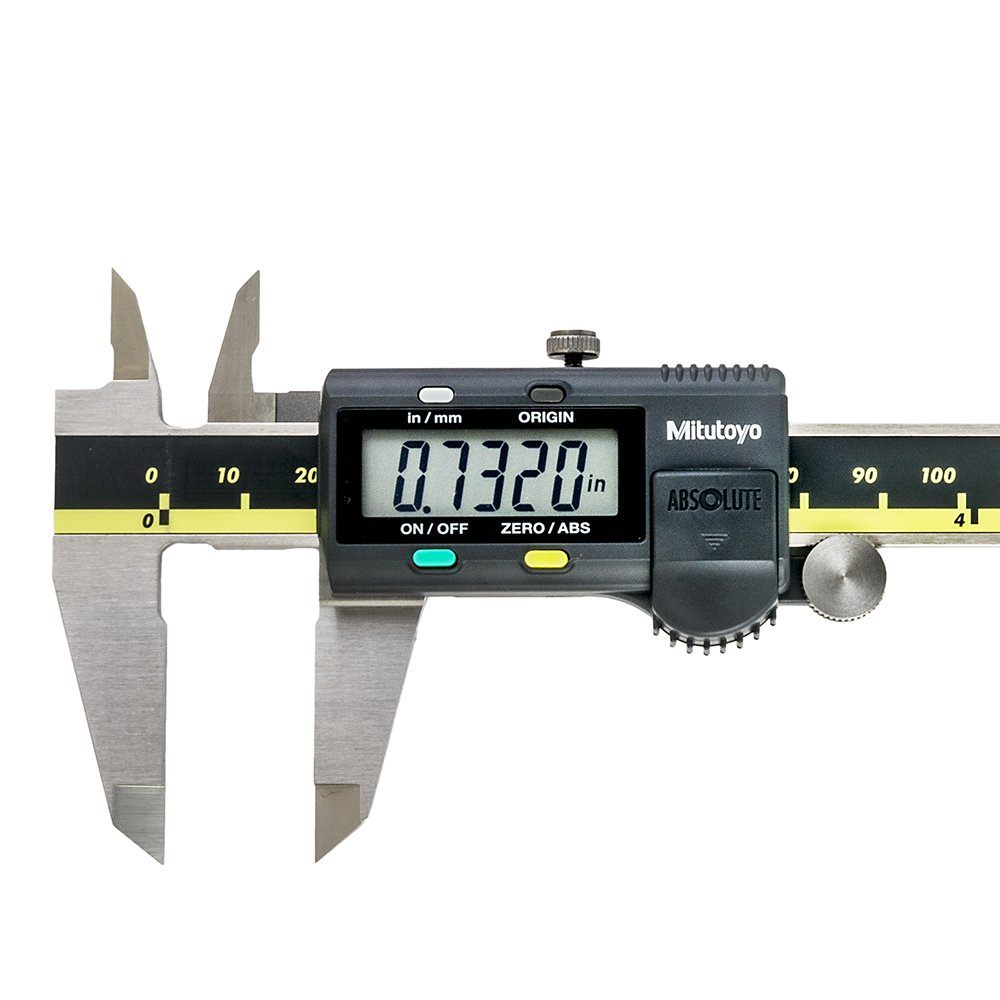
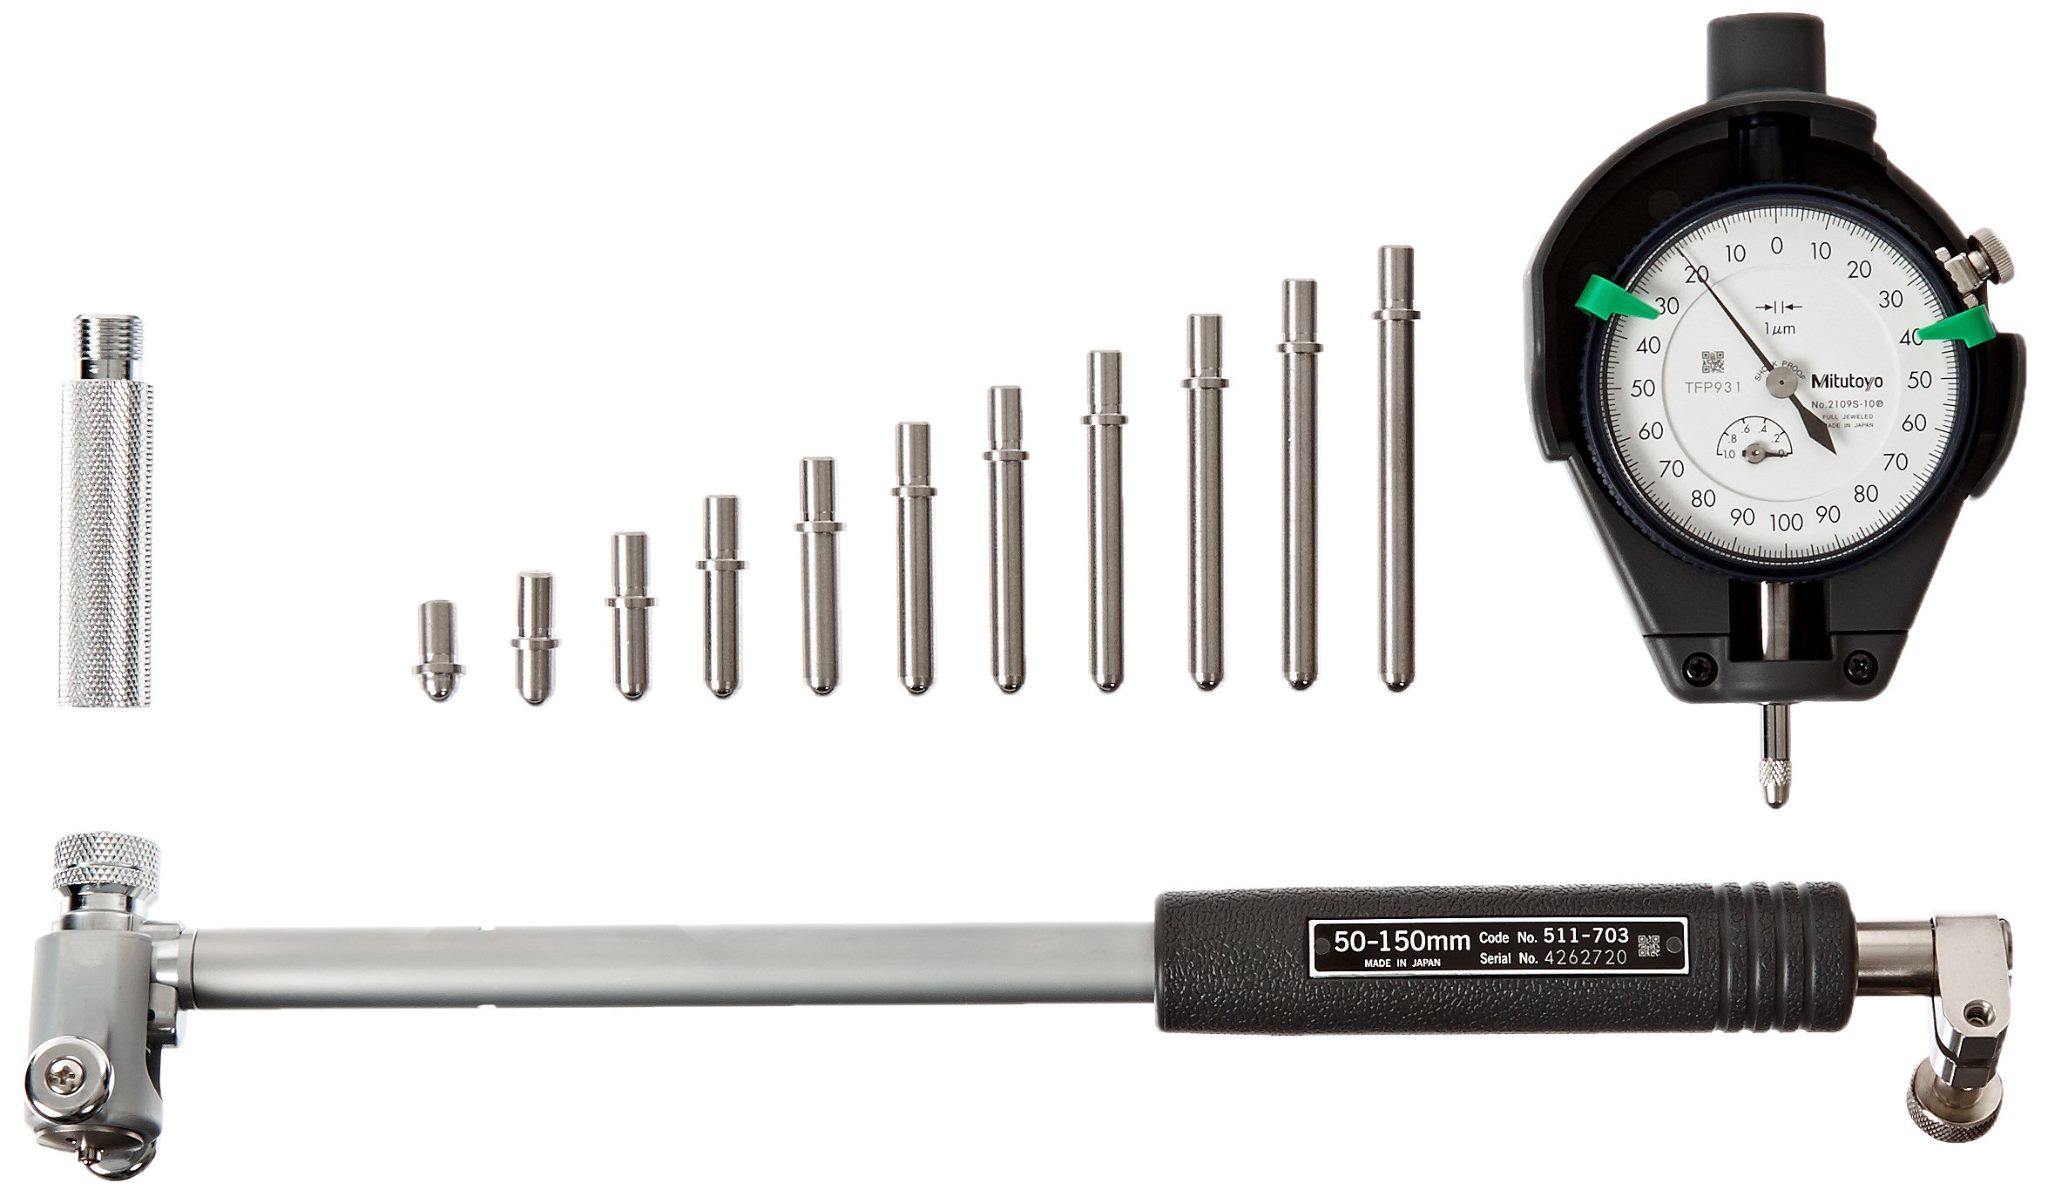
Quality at SPTI is not an inspection step — it is the operating system. Every die moves through a documented, ISO 9001:2015 certified process from drawing to dispatch.
management system
Five microns — roughly 1/14th the thickness of a human hair — held on critical punch and die profiles.
Design & strip layout
Lamination geometry, row count and stacking scheme engineered around your drawing and volume.
Wire-cut & jig boring
Punch, die and stripper profiles cut on Sodick wire-EDM; plate bores located on SIP jig boring.
Precision grinding
Studer cylindrical and Minini/Favretto surface grinding to final tolerance and finish.
Assembly & alignment
Guided die sets assembled with ball-cage guide posts for repeatable, rigid alignment.
Press try-out
Every die proven on our Yadon high-speed presses before release.
Inspection & after-sales
Parts verified with calibrated metrology; ongoing support and maintenance after delivery.
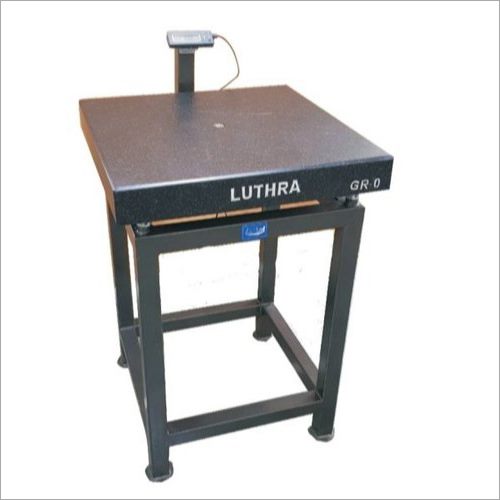
Trusted by industry leaders nationwide.
From appliance majors to automotive tier-ones and specialist stamping houses — across Haryana, Gujarat, Rajasthan, Delhi NCR, Karnataka and beyond.
Full client index · 53 partners
Leadership

Our journey is rooted in innovation, craftsmanship and customer trust. We are committed to precision-driven products and exceptional service — creating lasting value for every partner we serve.Satbir SinghFounder & Managing Director
Start your die.
Share your lamination drawing and volumes. Our engineering team will review the strip layout, technology and timeline, and respond with a detailed quotation.
- ContactSatbir Singh, Managing Director
- Phone+91 99993 22666
+91 99993 22661 - Emailsaiprecision18@gmail.com
- WorksPlot 7, Rishal Industrial Complex,
Jeevan Nagar, Gaunchi, Faridabad,
Haryana 121005, India - DirectionsOpen in Google Maps ↗